Application Review
Aerospace Engine / Turbine Components EDM Machining for Electrical Steel
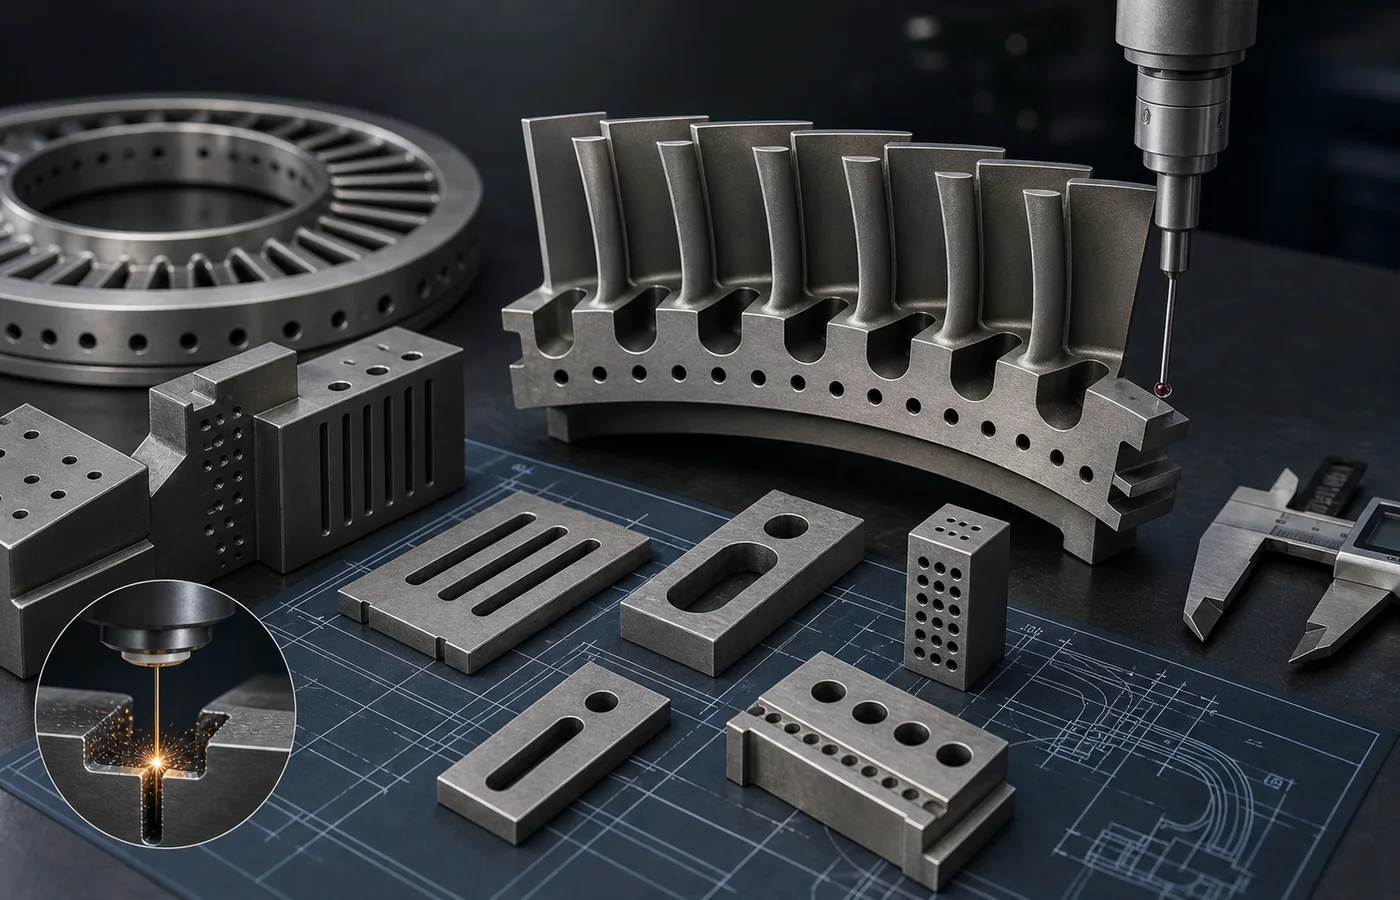
Electrical Steel can be reviewed for Aerospace Engine / Turbine Components, but the exact role of the part must justify the material’s strength, corrosion, wear, thermal, and documentation characteristics. In Aerospace Engine / Turbine Components, the functional requirements are high-temperature alloy profiles, cooling-hole features, sealing geometry and fatigue-sensitive surfaces. The material-specific concerns are that generic thick-part EDM language is inappropriate for lamination work.
Quick Answer
Electrical Steel can be considered for Aerospace Engine / Turbine Components, but first confirm that its strength, corrosion, wear, thermal, and documentation profile fits the actual part. Route each feature to Wire, Sinker, Small Hole, or Micro EDM from its access geometry.
Key Application Decisions
What's at Stake
In Aerospace Engine / Turbine Components, the part fails when recast, microcracks or edge damage on fatigue- and temperature-critical surfaces. Electrical Steel is thin magnetic steel where edge damage and interlaminar condition are functional requirements; its role must be justified by the actual load, environment, wear, temperature, corrosion, or contact requirement.
How to Get It Right
Use Electrical Steel only where its properties match the functional part. Route through profiles, blind forms, difficult holes, and miniature details to the appropriate EDM process, then define critical profiles, hole location, surface integrity, material certs, inspection reports. Compare the material with the alternatives listed below before freezing the drawing.
What Can Go Wrong
Using it as the primary service material can produce a dimensionally correct part that fails temperature, fatigue life, oxidation resistance, and surface-integrity acceptance because it is not a general structural or corrosion-resistant material and edge damage can change magnetic performance. A technically successful EDM cut does not correct a poor material choice. Keep Electrical Steel within this permitted role: motor laminations, magnetic test coupons, transformer profiles, and electromagnetic tooling.
How EDM Fits the Application
EDM is selected feature by feature for Aerospace Engine / Turbine Components: Wire for through profiles, Sinker for blind forms, Small Hole for difficult holes, and Micro EDM for miniature details. On Electrical Steel, the supplied condition determines support, finishing energy, post-processing, and inspection.
Electrical Steel Application Reference
| What matters | What to expect |
|---|---|
| Material behavior | thin magnetic steel where edge damage and interlaminar condition are functional requirements |
| Material-specific concern | generic thick-part EDM language is inappropriate for lamination work |
| Surface action | keep discharge energy low on thin laminations and inspect edge continuity rather than applying a generic polish requirement |
Aerospace Engine / Turbine Components Application Planning
| What matters | What to expect |
|---|---|
| Typical parts | turbine seals, cooling-hole components, heat-resistant alloy profiles, and precision engine fixtures |
| Functional requirement | high-temperature alloy profiles, cooling-hole features, sealing geometry and fatigue-sensitive surfaces |
| Main failure risk | recast, microcracks or edge damage on fatigue- and temperature-critical surfaces |
| Inspection focus | critical profiles, hole location, surface integrity, material certs, inspection reports |
| Planning context | Critical profiles and hole locations are commonly planned in the ±0.005–0.020 mm range, with selected functional surfaces using Ra 0.4–1.6 μm when required. |
Material Choices for This Application
Electrical Steel is electrically machinable, but it is a poor functional match for most Aerospace Engine / Turbine Components parts. The material offers controlled magnetic behavior in laminations and electromagnetic components, yet it is not a general structural or corrosion-resistant material and edge damage can change magnetic performance conflict with temperature, fatigue life, oxidation resistance, and surface-integrity acceptance. Restrict it to motor laminations, magnetic test coupons, transformer profiles, and electromagnetic tooling only when that role is explicitly separated from the primary service requirement. Consider these alternatives where the current material does not fit the functional role: Inconel 718 / 625 fits high-temperature strength and oxidation resistance for hot-section and sealing features; slow EDM and strict recast control on fatigue faces; Ti-6Al-4V fits high strength-to-weight ratio for cooler structural and compressor features; surface contamination and fatigue-sensitive recast require explicit acceptance; 15-5PH / 17-4PH fits stable high-strength fixtures and cooler engine hardware; aging condition must be stated; 2024 / 7075 aluminum fits lightweight non-hot structural or fixture parts; corrosion protection and residual-stress control are more important than heat resistance.
Functional Surface and Edge Control
Mark the Aerospace Engine / Turbine Components edges, contact, seal, wear, alignment, or cosmetic faces that carry the function. Inspect critical profiles, hole location, surface integrity, material certs, inspection reports separately. For Electrical Steel, manage the material-specific risks: Generic thick-part EDM language is inappropriate for lamination work. Do not approve the part from one broad Ra value.
Aerospace Engine / Turbine Components Buyer Checkpoints
- Identify the feature whose failure would cause recast, microcracks or edge damage on fatigue- and temperature-critical surfaces.
- State the exact Electrical Steel condition and define the datum and method for critical profiles, hole location, surface integrity, material certs, inspection reports.
- Send functional surface notes, quantity, drawing revision, and documentation needs before quotation.
Common Applications
- prototype turbine seals
- test-only cooling-hole components
- sacrificial heat-resistant alloy profiles
- nonfunctional precision engine fixtures
Limits and Better Alternatives
Main Limit
Electrical Steel compatibility does not select the EDM process or prove that the material is suitable for every Aerospace Engine / Turbine Components function.
Consider Another Route When
Consider Inconel 718, Inconel 625, and Inconel X-750 when their strength, corrosion, wear, temperature, or documentation profile fits the part better. Use conventional machining when the geometry is open and EDM adds no functional value.
Practical Next Step
For an EDM review of Aerospace Engine / Turbine Components in Electrical Steel, send the drawing, exact condition, critical feature, tolerance, functional surfaces, quantity, and the inspection or documentation requirements. If the material choice is uncertain, we can compare it with a better-fitting alloy before quotation.
Practical Takeaway
Electrical Steel can be used for Aerospace Engine / Turbine Components only where its material properties support the functional demand. Route each feature to the correct EDM process and release critical profiles, hole location, surface integrity, material certs, inspection reports with the functional surface requirements.
Check If This Applies to Your Project
Send application notes and a drawing for a project-specific feasibility check.
- Material: Electrical Steel
- Application: Aerospace Engine / Turbine Components
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.