Process & Material
Silver Wire EDM Feasibility Review
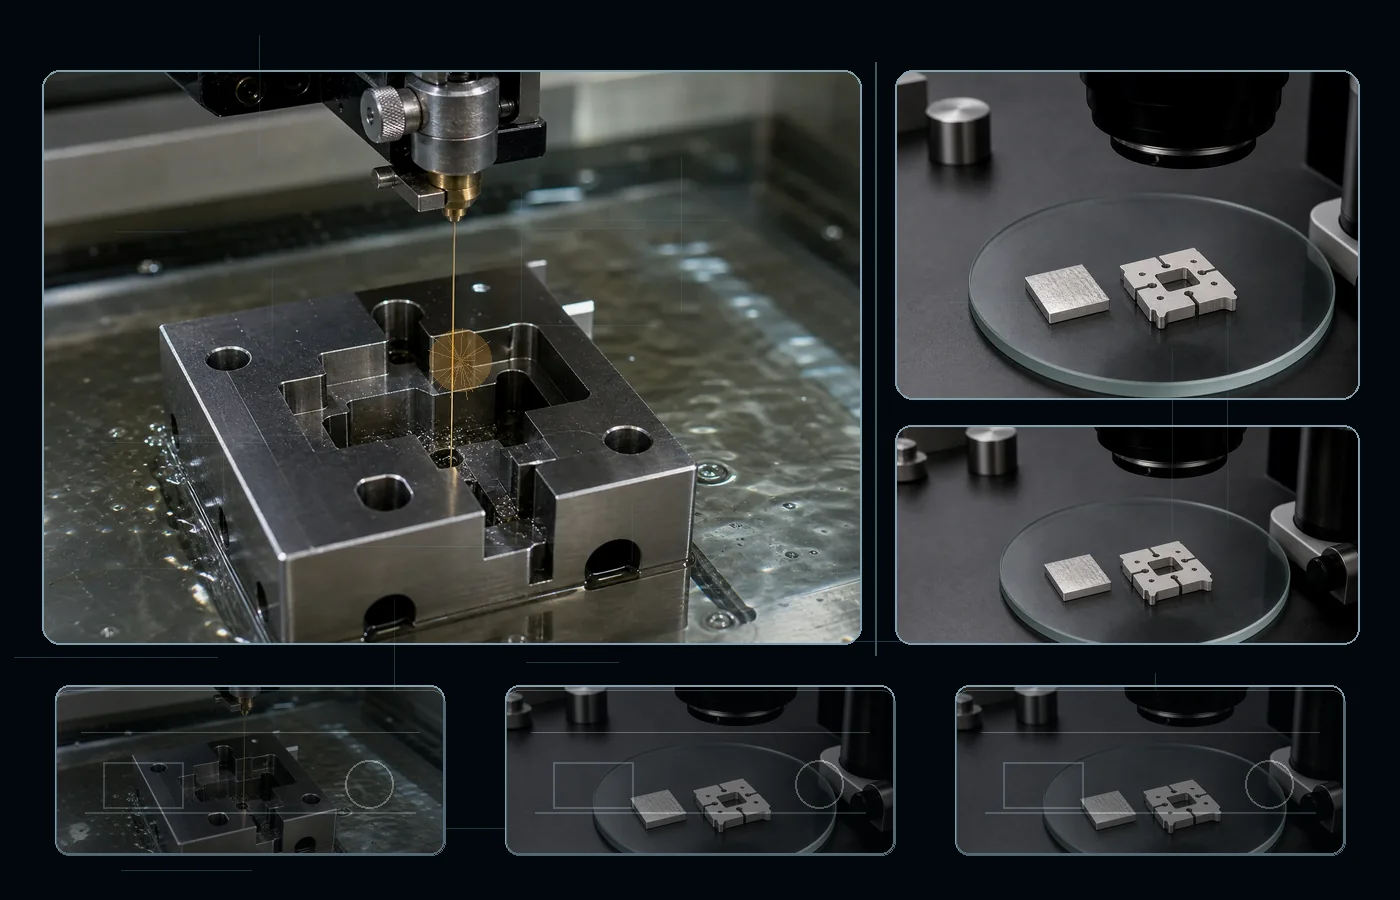
Silver can be machined with Wire EDM when the geometry matches through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls. Silver is the highest-conductivity common metal and a soft valuable material; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Wire EDM is suitable for Silver when the wire can pass completely through the workpiece from an edge or a start hole. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
The highest-conductivity common metal and a soft valuable material. In Wire EDM, the supplied condition changes stress release during the through cut, edge response to trim passes, and the final corrosion or surface-protection route.
Choosing the Right Condition
Choose Wire EDM for through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls. State the exact Silver condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Wire EDM, high heat flow, surface marking and material recovery affect setup more than electrical suitability. Between the rough cut and the final skim passes, offset compensation may remain correct at the top while the released section moves or the lower edge trails, with the highest consequence at high-value edges, recovered slugs and mark-sensitive surfaces. The Silver feature may therefore show profile error, surface marking or avoidable kerf loss on high-value material. For Silver, use protected fixturing, minimize unnecessary stock removal and maintain a controlled recovery and handling procedure. Inspect both cut edges and confirm the final profile after support tabs are removed; document geometry, handling marks, material loss and recovery records for Silver.
How Wire EDM Works on Silver
Wire EDM removes Silver along a continuous through-cut with a moving wire electrode. Wire tension, guide alignment, flushing and trim-pass offset control kerf, taper, verticality and internal corner radius as the profile opens. The route requires a complete wire path from an edge or start hole and does not produce blind cavities.
Wire EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls |
| Tolerance | ±0.005–0.025 mm |
| Surface finish | Ra 0.2–3.2 μm |
| Wire diameter | 0.10–0.30 mm planning range |
| Minimum internal corner | Approximately wire radius plus spark gap |
| Main limitation | Blind cavities and closed pockets are not wire-cut features. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| annealed | Use stable support and economical roughing. | Clamping and material condition can move delicate features. | Apply fine finishing only to functional faces. |
| work-hardened | Balance dimensional stability with feature-specific finishing. | Residual stress can shift thin sections or small details. | Identify wear, seal, fatigue, or contact surfaces. |
How This Material Behaves
Silver is very soft and has the highest electrical and thermal conductivity of common metals. In EDM, this means discharge energy is dissipated quickly and delicate edges can be marked during clamping, while fresh surfaces can tarnish before electrical assembly. Use broad clean support, stable fine-energy settings, and protect contact faces immediately after machining and cleaning. For Wire EDM, high heat flow, surface marking and material recovery affect setup more than electrical suitability. On open profiles, nonmarking support, minimum kerf loss and controlled slug recovery matter as much as profile accuracy.
Surface Integrity and Post-Process
For Wire EDM on Silver, use protected fixturing, controlled finishing and recovery procedures for cut-off material. Separate the rough cut from skim cuts and apply the fine finish only to functional edges. Inspect roughness, edge rounding, recast and corrosion or fatigue requirements after the final pass; include polishing, coating or protection allowance wherever it changes final size.
Silver Wire EDM Checkpoints
- Confirm that the feature matches through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls.
- State the supplied condition: annealed and work-hardened.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- fine contacts
- watch and jewelry details
- laboratory electrodes
- punches and die inserts
- precision profile gauges
- gear and spline outlines
Limits and Better Alternatives
Main Limit
Blind cavities and closed pockets are not wire-cut features because the wire needs a continuous through path. On Silver, high heat flow, surface marking and material recovery affect setup more than electrical suitability; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use Sinker EDM for blind cavities, CNC machining for accessible open geometry, or laser cutting when thin-sheet speed matters more than EDM edge quality.
Practical Next Step
Send the Silver drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Wire EDM with the adjacent EDM or conventional process.
Practical Takeaway
Silver is compatible with Wire EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Technical Reference
Use the values as planning references and define the functional requirement on the controlled drawing.
Use This Guide to Prepare Your RFQ
Contact us when your drawing and requirements are ready for review.
- Process: Wire EDM
- Material: Silver
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.