Process & Material
Silver Small Hole EDM Drilling Feasibility Review
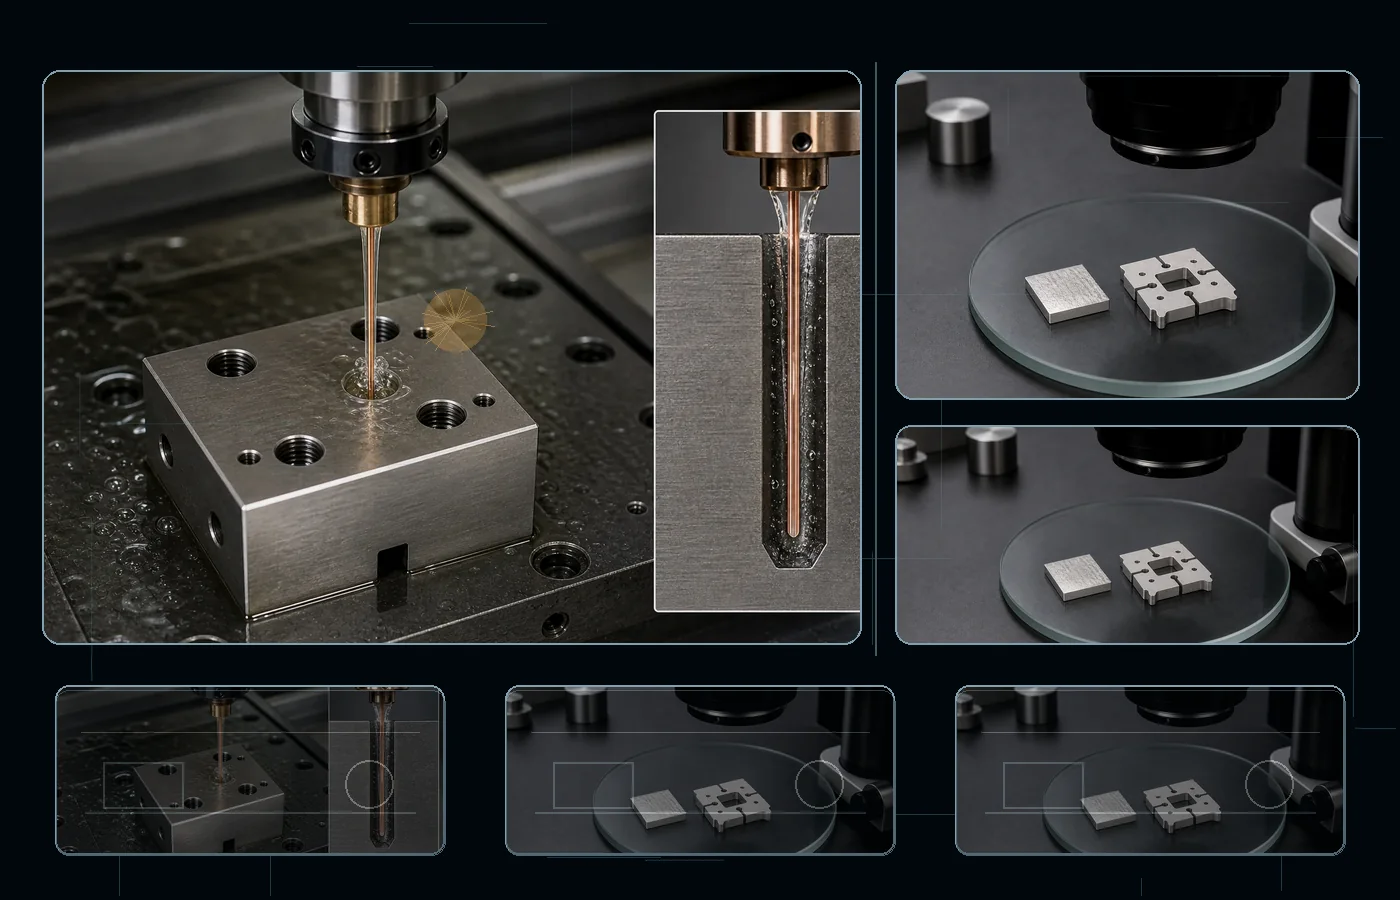
Silver can be machined with Small Hole EDM when the geometry matches small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys. Silver is the highest-conductivity common metal and a soft valuable material; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Small Hole EDM is suitable for Silver when the feature is a small, deep, angled, cooling, vent, or start hole in conductive material. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
The highest-conductivity common metal and a soft valuable material. In Small Hole EDM, the supplied condition changes bore stability, breakthrough quality, wall finish, and the inspection plan for straightness and position.
Choosing the Right Condition
Choose Small Hole EDM for small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys. State the exact Silver condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Small Hole EDM, high heat flow, surface marking and material recovery affect setup more than electrical suitability. The far end of the hole can drift even when the entry diameter and start position remain stable during the final portion of a high-aspect-ratio hole; acceptance must focus on high-value edges, recovered slugs and mark-sensitive surfaces. On Silver, the resulting defect can be exit deformation, contact-surface damage or avoidable material loss. For Silver, use protected fixturing, minimize unnecessary stock removal and maintain a controlled recovery and handling procedure. Inspect entry, exit, taper, position and wall condition independently; document geometry, handling marks, material loss and recovery records for Silver.
How Small Hole EDM Works on Silver
Small Hole EDM advances a rotating tubular electrode through Silver while dielectric exits at the cutting tip. Electrode wear, runout, internal flushing, true hole depth and breakthrough support control entry-to-exit diameter, taper, straightness and wall condition. Hole diameter, depth and depth-to-diameter ratio—not stock thickness alone—define the process limit.
Small Hole EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys |
| Tolerance | ±0.010–0.050 mm |
| Surface finish | Hole-wall finish is feature-dependent |
| Typical diameter | About 0.3–3.0 mm for ordinary planning |
| Depth driver | Depth-to-diameter ratio, straightness, and breakthrough |
| Main limitation | Very small diameter combined with extreme depth may require specialized equipment, staged electrodes, and dedicated metrology. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| annealed | Use stable support and economical roughing. | Clamping and material condition can move delicate features. | Apply fine finishing only to functional faces. |
| work-hardened | Balance dimensional stability with feature-specific finishing. | Residual stress can shift thin sections or small details. | Identify wear, seal, fatigue, or contact surfaces. |
How This Material Behaves
Silver is very soft and has the highest electrical and thermal conductivity of common metals. In EDM, this means discharge energy is dissipated quickly and delicate edges can be marked during clamping, while fresh surfaces can tarnish before electrical assembly. Use broad clean support, stable fine-energy settings, and protect contact faces immediately after machining and cleaning. For Small Hole EDM, high heat flow, surface marking and material recovery affect setup more than electrical suitability. For small holes, exit deformation, material recovery and protection of functional contact surfaces must be planned before cutting.
Surface Integrity and Post-Process
For Small Hole EDM on Silver, use protected fixturing, controlled finishing and recovery procedures for cut-off material. Reduce discharge energy near final size and breakthrough, then evaluate entry, exit, taper and wall condition separately. For fatigue-, flow- or seal-critical holes, specify recast acceptance or post-process cleaning and finishing instead of relying on diameter alone.
Silver Small Hole EDM Checkpoints
- Confirm that the feature matches small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys.
- State the supplied condition: annealed and work-hardened.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- fine contacts
- watch and jewelry details
- laboratory electrodes
- turbine-blade cooling holes
- mold and die vent holes
- injector and nozzle holes
Limits and Better Alternatives
Main Limit
Hole depth, diameter, aspect ratio, flushing, and breakthrough quality—not stock thickness alone—set the practical limit. On Silver, high heat flow, surface marking and material recovery affect setup more than electrical suitability; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use mechanical drilling when the tool can reach economically, laser drilling for suitable thin geometry, or Micro EDM for smaller precision holes.
Practical Next Step
Send the Silver drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Small Hole EDM with the adjacent EDM or conventional process.
Practical Takeaway
Silver is compatible with Small Hole EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Technical Reference
Use the values as planning references and define the functional requirement on the controlled drawing.
Use This Guide to Prepare Your RFQ
Contact us when your drawing and requirements are ready for review.
- Process: Small Hole EDM
- Material: Silver
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.