Process & Material
Molybdenum Small Hole EDM Drilling Feasibility Review
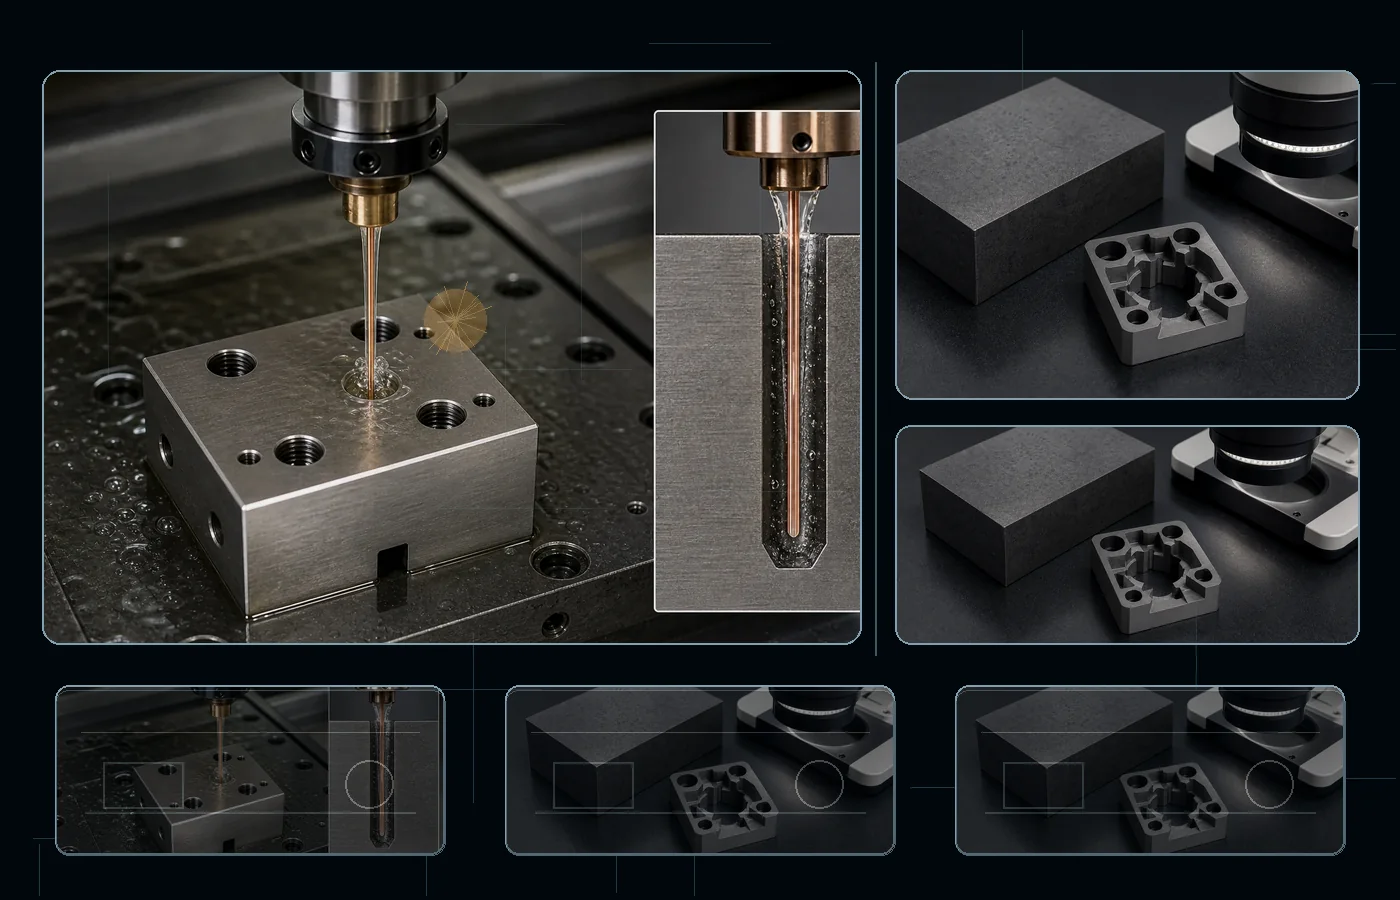
Molybdenum can be machined with Small Hole EDM when the geometry matches small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys. Molybdenum is a refractory metal with high melting temperature, good conductivity and limited room-temperature ductility in some forms; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Small Hole EDM is suitable for Molybdenum when the feature is a small, deep, angled, cooling, vent, or start hole in conductive material. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
A refractory metal with high melting temperature, good conductivity and limited room-temperature ductility in some forms. In Small Hole EDM, the supplied condition changes bore stability, breakthrough quality, wall finish, and the inspection plan for straightness and position.
Choosing the Right Condition
Choose Small Hole EDM for small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys. State the exact Molybdenum condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Small Hole EDM, brittle edge behavior, grain direction and thin-feature support require conservative energy. While pressure and electrode condition change along the true hole depth, electrode shortening and debris transport can change taper, straightness and wall condition together, with the highest consequence at grain boundaries, brittle rims and subsurface damage zones. The Molybdenum feature may therefore show exit-rim chipping and hidden wall damage despite acceptable entry size. For Molybdenum, use conservative discharge energy, strong local support and microscopic inspection of edges and subsurface damage. Inspect entry, exit, taper, position and wall condition independently; document geometry, chipping, grain pullout and subsurface cracking for Molybdenum.
How Small Hole EDM Works on Molybdenum
Small Hole EDM advances a rotating tubular electrode through Molybdenum while dielectric exits at the cutting tip. Electrode wear, runout, internal flushing, true hole depth and breakthrough support control entry-to-exit diameter, taper, straightness and wall condition. Hole diameter, depth and depth-to-diameter ratio—not stock thickness alone—define the process limit.
Small Hole EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys |
| Tolerance | ±0.010–0.050 mm |
| Surface finish | Hole-wall finish is feature-dependent |
| Typical diameter | About 0.3–3.0 mm for ordinary planning |
| Depth driver | Depth-to-diameter ratio, straightness, and breakthrough |
| Main limitation | Very small diameter combined with extreme depth may require specialized equipment, staged electrodes, and dedicated metrology. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| as-sintered or supplied condition | Use low-force fixturing and conservative discharge energy. | Brittle edges can chip or binder-rich zones can erode unevenly. | Inspect edge breakout and surface integrity rather than Ra alone. |
| stress-relieved or recrystallized | Use stable support and reduced energy on finished stock. | Grinding stress or porosity can cause local cracking. | Apply selective polishing or lapping where practical. |
How This Material Behaves
Molybdenum is a refractory metal with high melting temperature but limited room-temperature ductility. In EDM, this means fine corners can chip and thermal gradients can create microcracks even though the material is electrically machinable. Use low-energy finishing, avoid unsupported sharp edges, and verify crack-sensitive surfaces with microscopy rather than visual inspection alone. For Small Hole EDM, brittle edge behavior, grain direction and thin-feature support require conservative energy. At breakthrough, the exit rim and hole wall are the critical locations for chipping, pullout and hidden subsurface damage.
Surface Integrity and Post-Process
For Small Hole EDM on Molybdenum, use conservative energy, strong support and inspection focused on edge chipping and subsurface damage. Reduce discharge energy near final size and breakthrough, then evaluate entry, exit, taper and wall condition separately. For fatigue-, flow- or seal-critical holes, specify recast acceptance or post-process cleaning and finishing instead of relying on diameter alone.
Molybdenum Small Hole EDM Checkpoints
- Confirm that the feature matches small through holes, deep holes, angled holes, cooling holes, vent holes, and start holes in hard or heat-resistant alloys.
- State the supplied condition: as-sintered or supplied condition and stress-relieved or recrystallized.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- wear inserts
- high-temperature contacts
- hard-metal nozzles
- turbine-blade cooling holes
- mold and die vent holes
- injector and nozzle holes
Limits and Better Alternatives
Main Limit
Hole depth, diameter, aspect ratio, flushing, and breakthrough quality—not stock thickness alone—set the practical limit. On Molybdenum, brittle edge behavior, grain direction and thin-feature support require conservative energy; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use mechanical drilling when the tool can reach economically, laser drilling for suitable thin geometry, or Micro EDM for smaller precision holes.
Practical Next Step
Send the Molybdenum drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Small Hole EDM with the adjacent EDM or conventional process.
Practical Takeaway
Molybdenum is compatible with Small Hole EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Technical Reference
Use the values as planning references and define the functional requirement on the controlled drawing.
Use This Guide to Prepare Your RFQ
Contact us when your drawing and requirements are ready for review.
- Process: Small Hole EDM
- Material: Molybdenum
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.