Process & Material
Maraging Steel Micro EDM Feasibility Review
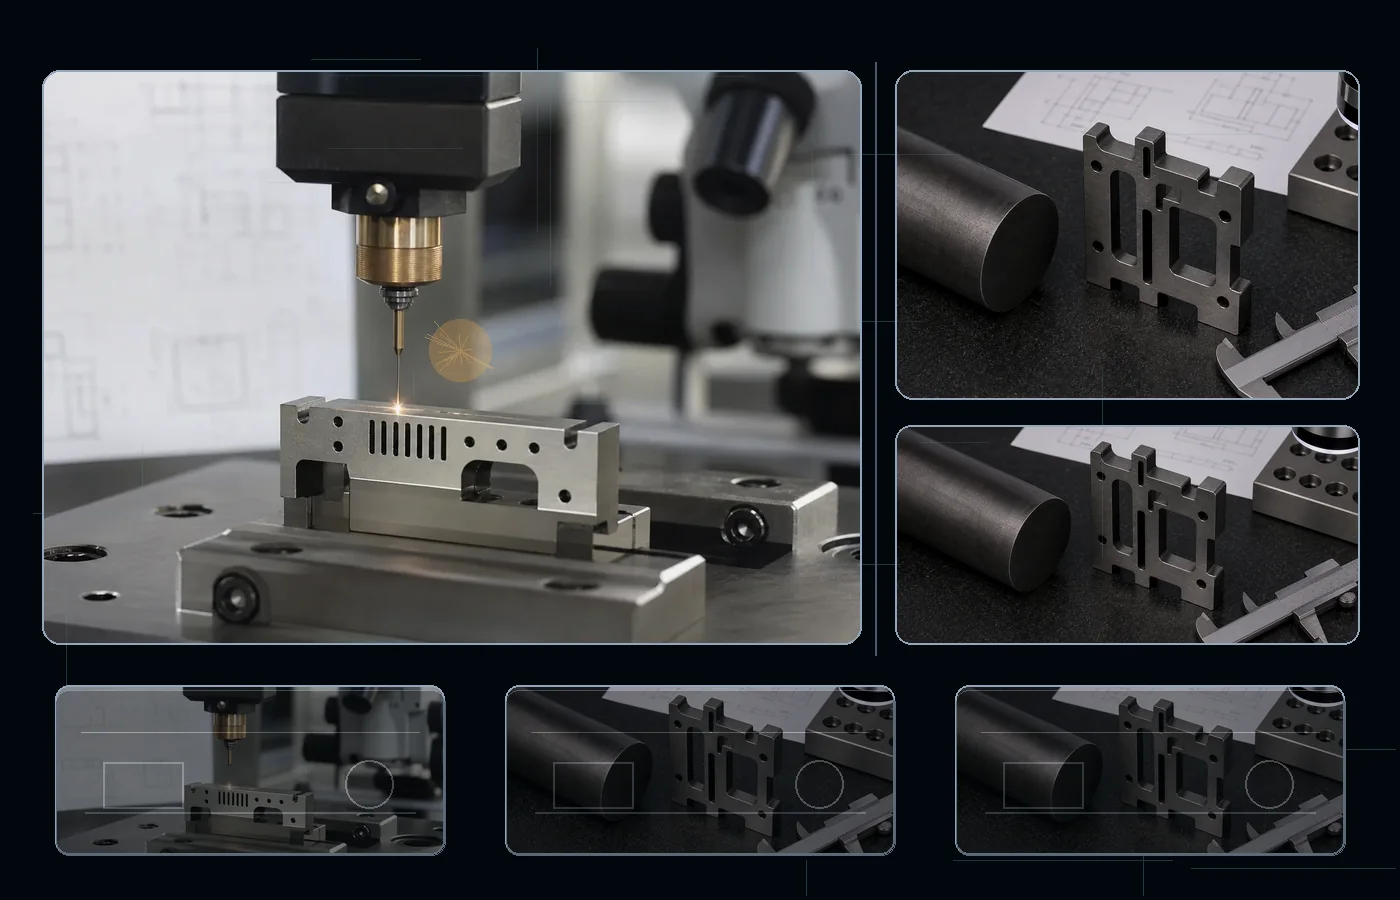
Maraging Steel can be machined with Micro EDM when the geometry matches micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details. Maraging Steel is a low-carbon high-nickel steel strengthened by aging rather than carbon hardening; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Micro EDM is suitable for Maraging Steel when the feature is a micro hole, micro slot, miniature cavity, fine pin, or other sub-millimeter detail. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
A low-carbon high-nickel steel strengthened by aging rather than carbon hardening. In Micro EDM, the supplied condition directly changes discharge stability, electrode wear, edge quality, and the finishing plan—especially at micro scale.
Choosing the Right Condition
Choose Micro EDM for micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details. State the exact Maraging Steel condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Micro EDM, solution-treated and aged states have different stress and hardness behavior, especially on precision thin sections. Edge rounding and tool wear can be indistinguishable from true dimensional error without suitable metrology as micro-flushing, temperature and metrology become part of the same tolerance chain; acceptance must focus on fatigue-loaded edges and free-state datums. On Maraging Steel, the resulting defect can be feature drift accompanied by a surface layer that is unacceptable for cyclic loading. For Maraging Steel, balance material removal, use lower-energy finishing, and state the allowable recast or microcrack condition on service edges. Verify size, pitch, edge continuity and surface condition under the same inspection plan; document free-state geometry, recast and the fatigue-critical edge condition for Maraging Steel.
How Micro EDM Works on Maraging Steel
Micro EDM uses a very small electrode and low discharge energy to machine miniature features in Maraging Steel. Electrode wear, spark-gap stability, micro-flushing, temperature control and measurement resolution consume a significant share of the available tolerance. The local feature size and aspect ratio—not the overall workpiece size—must define the route.
Micro EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details |
| Tolerance | ±0.002–0.010 mm |
| Surface finish | Ra 0.1–1.6 μm |
| Feature scale | Sub-millimeter holes, slots, and cavities |
| Primary micro limit | Electrode wear and measurement resolution |
| Main limitation | Loose-tolerance or easily accessible features are rarely economical with Micro EDM. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| solution annealed | Use economical roughing with stable support. | Soft sections can mark, bow, or release machining stress. | Protect exposed EDM faces from corrosion and reserve fine finishing for functional areas. |
| aged condition | Sequence rough and finish cuts around the datum scheme. | Residual stress can move thin walls or narrow webs. | Use lower-energy finishing on fatigue and wear faces. |
| stress-relieved finished condition | Use conservative energy and stress-aware fixturing. | Hard edges can microcrack and retain a deeper white layer. | Apply trim passes or recast removal where fatigue or wear matters. |
How This Material Behaves
Maraging steel gains very high strength from aging rather than high carbon content. In EDM, this means the solution-treated and aged conditions can differ in hardness, residual stress, and recast response, while fatigue-critical edges remain sensitive to a brittle resolidified layer. State the aging condition, finish after major stress changes are complete, and remove or limit recast on load-bearing surfaces. For Micro EDM, solution-treated and aged states have different stress and hardness behavior, especially on precision thin sections. At micro scale, hardened condition, recast and measurement uncertainty all consume the same limited tolerance budget.
Surface Integrity and Post-Process
For Micro EDM on Maraging Steel, critical fatigue surfaces benefit from lower-energy finishing and a clear recast-layer requirement. Use low-energy finishing and account for electrode replacement or calibration before final sizing. Specify edge, recast and post-process requirements only on functional microfeatures, and use metrology that can distinguish true size from edge rounding and surface residue.
Maraging Steel Micro EDM Checkpoints
- Confirm that the feature matches micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details.
- State the supplied condition: solution annealed, aged condition, and stress-relieved finished condition.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- high-strength inserts
- shafts and profiles
- fixtures
- micro holes
- micro slots
- miniature cavities
Limits and Better Alternatives
Main Limit
Loose-tolerance or easily accessible features are rarely economical with Micro EDM. On Maraging Steel, solution-treated and aged states have different stress and hardness behavior, especially on precision thin sections; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use conventional EDM for larger features, precision laser processing for suitable thin geometry, or mechanical micro-drilling where a tool can reach.
Practical Next Step
Send the Maraging Steel drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Micro EDM with the adjacent EDM or conventional process.
Practical Takeaway
Maraging Steel is compatible with Micro EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Additional Project Information
Include application, destination and end-use notes together with the material, quantity and drawing requirements.
Project Details for Technical Review
Include application and end-use notes when they affect material, inspection, documentation, or export review.
- Process: Micro EDM
- Material: Maraging Steel
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.
Frequently Asked Questions
Can Maraging Steel be machined with Micro EDM?
Yes, when the feature is a micro hole, micro slot, miniature cavity, fine pin, or other sub-millimeter detail. Maraging Steel is electrically conductive and the final route follows the feature geometry and supplied condition.
What controls Micro EDM on Maraging Steel?
The main process controls are electrode wear, feature-to-electrode ratio, micro-flushing, aspect ratio, edge radius, thermal stability, and measurement resolution. The Maraging Steel condition adds dimensional-stability and surface-integrity requirements.
What is the main risk?
For Micro EDM, solution-treated and aged states have different stress and hardness behavior, especially on precision thin sections. Edge rounding and tool wear can be indistinguishable from true dimensional error without suitable metrology as micro-flushing, temperature and metrology become part of the same tolerance chain; acceptance must focus on fatigue-loaded edges and free-state datums. On Maraging Steel, the resulting defect can be feature drift accompanied by a surface layer that is unacceptable for cyclic loading. For Maraging Steel, balance material removal, use lower-energy finishing, and state the allowable recast or microcrack condition on service edges. Verify size, pitch, edge continuity and surface condition under the same inspection plan; document free-state geometry, recast and the fatigue-critical edge condition for Maraging Steel.
What should I send for review?
Send the drawing, exact Maraging Steel condition, controlled geometry, tolerance, functional surface requirements, quantity, and inspection expectations. If any item is undecided, send what you have and we will help complete the review.