Process & Material
Gold Micro EDM Feasibility Review
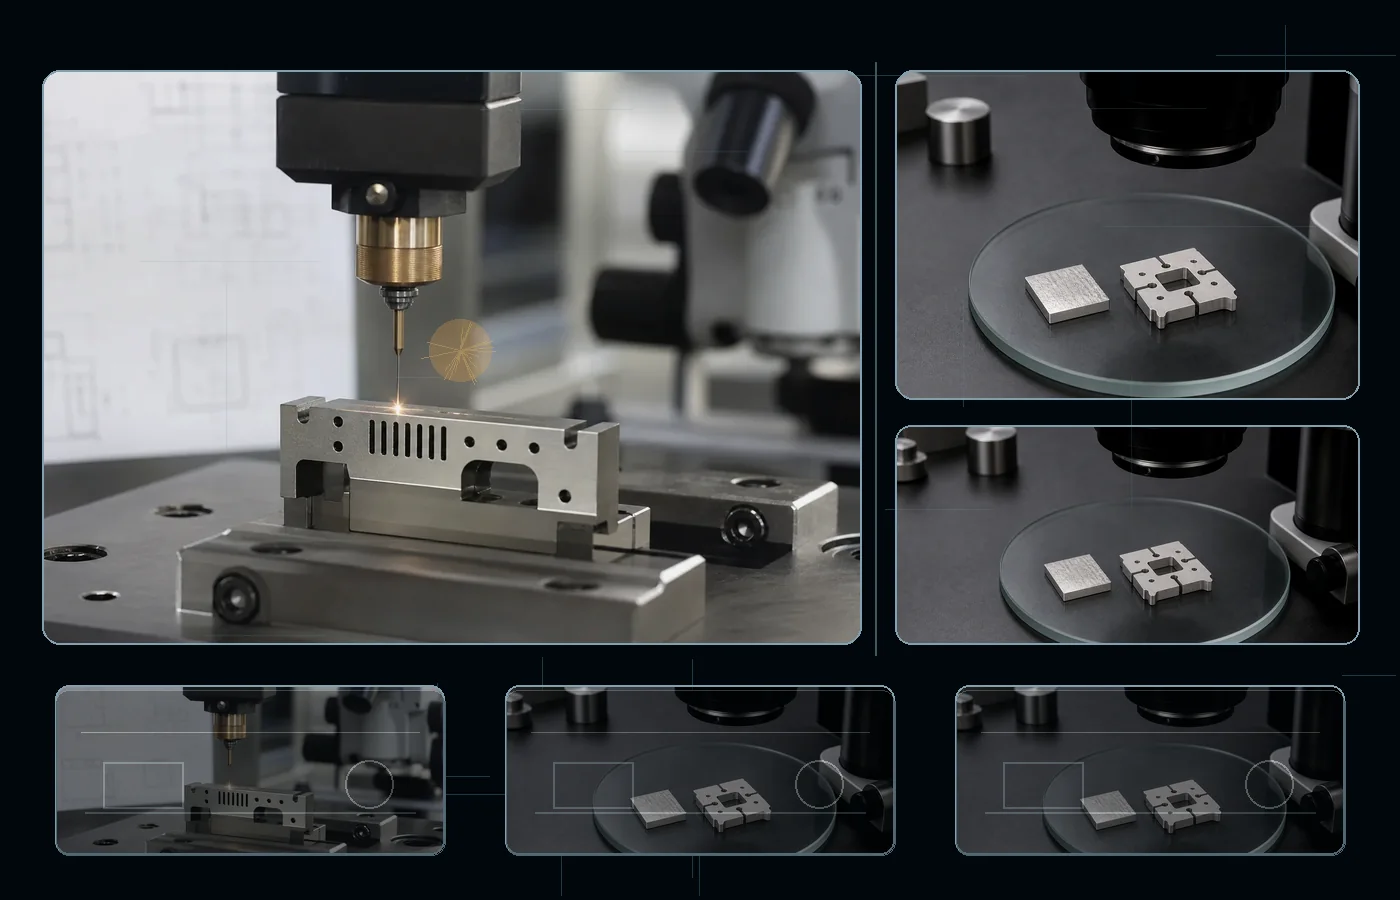
Gold can be machined with Micro EDM when the geometry matches micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details. Gold is a very soft, dense and highly conductive precious metal; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Micro EDM is suitable for Gold when the feature is a micro hole, micro slot, miniature cavity, fine pin, or other sub-millimeter detail. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
A very soft, dense and highly conductive precious metal. In Micro EDM, the supplied condition directly changes discharge stability, electrode wear, edge quality, and the finishing plan—especially at micro scale.
Choosing the Right Condition
Choose Micro EDM for micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details. State the exact Gold condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Micro EDM, surface marking, thin-feature distortion and material recovery can matter more than discharge stability. Electrode wear, debris and spark-gap variation can move size and pitch together during the final sizing of a sub-millimeter slot, hole or datum feature, especially around high-value edges, recovered slugs and mark-sensitive surfaces. The practical failure in Gold is handling marks, overcut and material loss acting at the same scale as the feature. For Gold, use protected fixturing, minimize unnecessary stock removal and maintain a controlled recovery and handling procedure. Control electrode replacement, cleaning and measurement as one final-sizing sequence; document geometry, handling marks, material loss and recovery records for Gold.
How Micro EDM Works on Gold
Micro EDM uses a very small electrode and low discharge energy to machine miniature features in Gold. Electrode wear, spark-gap stability, micro-flushing, temperature control and measurement resolution consume a significant share of the available tolerance. The local feature size and aspect ratio—not the overall workpiece size—must define the route.
Micro EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details |
| Tolerance | ±0.002–0.010 mm |
| Surface finish | Ra 0.1–1.6 μm |
| Feature scale | Sub-millimeter holes, slots, and cavities |
| Primary micro limit | Electrode wear and measurement resolution |
| Main limitation | Loose-tolerance or easily accessible features are rarely economical with Micro EDM. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| annealed | Use stable support and economical roughing. | Clamping and material condition can move delicate features. | Apply fine finishing only to functional faces. |
| work-hardened | Balance dimensional stability with feature-specific finishing. | Residual stress can shift thin sections or small details. | Identify wear, seal, fatigue, or contact surfaces. |
| finished or plated condition | Use conservative energy and selective inspection. | Finished or hardened surfaces can be sensitive to edge damage and recast. | Use lower-energy finishing or post-processing where function requires it. |
How This Material Behaves
Gold is extremely soft, dense, conductive, and costly. In EDM, this means the part can be damaged by clamping or handling before spark erosion becomes the limiting factor, and unnecessary overcut directly increases material loss. Use broad nonmarking support, minimize roughing stock, capture the final geometry with few controlled passes, and keep contact-surface cleanliness in the release plan. For Micro EDM, surface marking, thin-feature distortion and material recovery can matter more than discharge stability. At micro scale, handling marks and overcut can equal the feature tolerance, so recovery, cleaning and metrology must be integrated with the final burn.
Surface Integrity and Post-Process
For Micro EDM on Gold, use protected fixturing, controlled finishing and recovery procedures for cut-off material. Use low-energy finishing and account for electrode replacement or calibration before final sizing. Specify edge, recast and post-process requirements only on functional microfeatures, and use metrology that can distinguish true size from edge rounding and surface residue.
Gold Micro EDM Checkpoints
- Confirm that the feature matches micro holes, micro slots, miniature cavities, fine pins, and sub-millimeter precision details.
- State the supplied condition: annealed, work-hardened, and finished or plated condition.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- fine contacts
- watch and jewelry details
- laboratory electrodes
- micro holes
- micro slots
- miniature cavities
Limits and Better Alternatives
Main Limit
Loose-tolerance or easily accessible features are rarely economical with Micro EDM. On Gold, surface marking, thin-feature distortion and material recovery can matter more than discharge stability; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use conventional EDM for larger features, precision laser processing for suitable thin geometry, or mechanical micro-drilling where a tool can reach.
Practical Next Step
Send the Gold drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Micro EDM with the adjacent EDM or conventional process.
Practical Takeaway
Gold is compatible with Micro EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Technical Reference
Use the values as planning references and define the functional requirement on the controlled drawing.
Use This Guide to Prepare Your RFQ
Contact us when your drawing and requirements are ready for review.
- Process: Micro EDM
- Material: Gold
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.