Process & Material
Cobalt Chrome Sinker EDM Feasibility Review
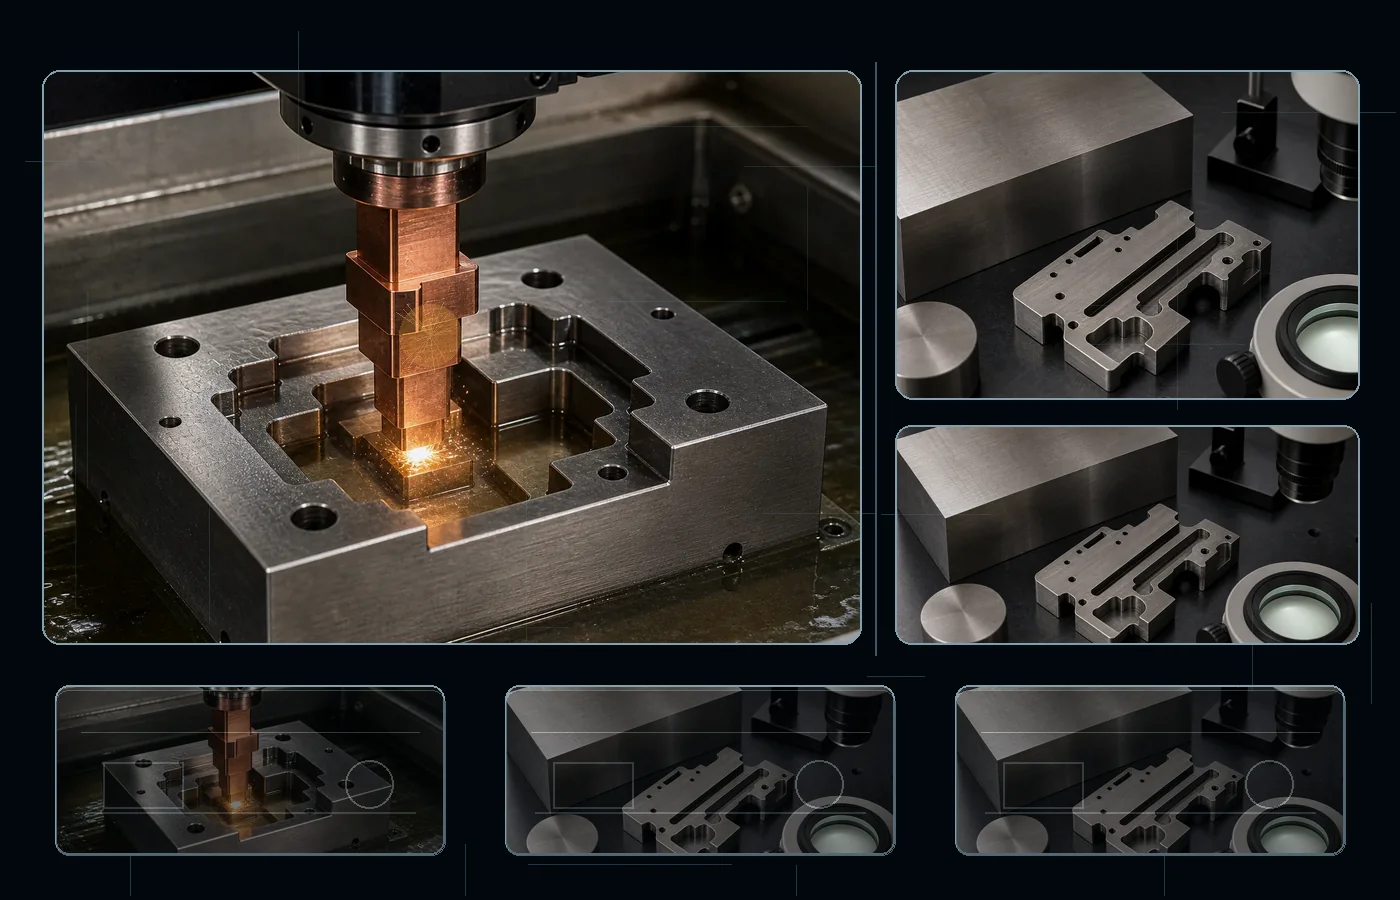
Cobalt Chrome can be machined with Sinker EDM when the geometry matches blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach. Cobalt Chrome is a hard corrosion-resistant cobalt alloy used for wear, medical and high-temperature features; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Sinker EDM is suitable for Cobalt Chrome when the feature is a blind cavity, rib, pocket, or internal form that a shaped electrode can reach from one side. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
A hard corrosion-resistant cobalt alloy used for wear, medical and high-temperature features. In Sinker EDM, the supplied condition changes electrode wear, cavity-floor consistency, corner growth, and the finishing strategy—especially on deep ribs and textured surfaces.
Choosing the Right Condition
Choose Sinker EDM for blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach. State the exact Cobalt Chrome condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Sinker EDM, brittle edge behavior and fatigue-critical surfaces make recast and microcrack review important. Orbit, local heating and electrode wear can shift wall size while dishing the floor as roughing transitions to final orbit and floor sizing, especially around wear, medical and cyclically loaded edge features. The practical failure in Cobalt Chrome is local cracking and floor-size error in a wear- or medical-critical cavity. For Cobalt Chrome, use conservative energy, protect sharp edges and define microscopic surface-integrity acceptance where service life depends on it. Inspect wall size, floor depth and corner condition as separate acceptance items; document geometry, edge continuity and microscopic fatigue-critical damage for Cobalt Chrome.
How Sinker EDM Works on Cobalt Chrome
Sinker EDM reproduces a shaped electrode as a blind cavity in Cobalt Chrome. Electrode material, wear, orbit, pulse energy and debris evacuation control wall size, floor depth, corner definition and surface condition. Where final size or texture is critical, roughing and finishing electrodes should be planned as separate operations.
Sinker EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach |
| Tolerance | ±0.008–0.030 mm |
| Surface finish | Ra 0.2–6.3 μm |
| Electrode choice | Graphite or copper selected from cavity, finish, and wear needs |
| Primary cavity limit | Depth, rib width, access, and debris evacuation |
| Main limitation | Electrode access and debris evacuation limit deep, narrow blind geometry. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| solution annealed | Use stable support and conservative energy. | High-temperature alloys can retain a hard recast layer. | Identify fatigue and hot-section faces before finishing. |
| cold-worked or stabilized | Account for cold-work and service stress. | Thin features can move and electrode wear can grow corners. | Use low-energy finishing and selective metallurgical inspection. |
| age-hardened or service condition | Use the final aged or service condition only with explicit surface requirements. | Microcracks and tensile residual stress can reduce fatigue life. | Remove or limit recast on fatigue-critical faces. |
How This Material Behaves
Cobalt-chrome alloys combine high hardness, wear resistance, and low thermal conductivity. In EDM, this means heat remains concentrated near the discharge zone, increasing recast and microcrack risk on fatigue, wear, or medical surfaces. Use progressive low-energy finishing, keep edges well supported, and specify recast removal or metallographic verification on critical faces. For Sinker EDM, brittle edge behavior and fatigue-critical surfaces make recast and microcrack review important. In deep ribs and blind cavities, heat concentration, debris retention and electrode wear can combine at the floor and corners.
Surface Integrity and Post-Process
For Sinker EDM on Cobalt Chrome, use lower-energy finishing and inspect critical surfaces when fatigue, sealing or corrosion performance is specified. Use roughing and finishing electrodes separately where cavity size or texture is controlled. Apply polishing, lapping or recast removal only to named functional faces, and inspect wall, floor and corner condition after the final surface operation.
Cobalt Chrome Sinker EDM Checkpoints
- Confirm that the feature matches blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach.
- State the supplied condition: solution annealed, cold-worked or stabilized, and age-hardened or service condition.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- turbine and energy features
- corrosion-resistant inserts
- precision seals
- mold cavities
- blind pockets
- deep ribs
Limits and Better Alternatives
Main Limit
Electrode access and debris evacuation limit deep, narrow blind geometry. On Cobalt Chrome, brittle edge behavior and fatigue-critical surfaces make recast and microcrack review important; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use Wire EDM for through profiles, CNC machining for open cavities with tool access, or grinding for simple flat precision surfaces.
Practical Next Step
Send the Cobalt Chrome drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Sinker EDM with the adjacent EDM or conventional process.
Practical Takeaway
Cobalt Chrome is compatible with Sinker EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Additional Project Information
Include application, destination and end-use notes together with the material, quantity and drawing requirements.
Project Details for Technical Review
Include application and end-use notes when they affect material, inspection, documentation, or export review.
- Process: Sinker EDM
- Material: Cobalt Chrome
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.
Frequently Asked Questions
Can Cobalt Chrome be machined with Sinker EDM?
Yes, when the feature is a blind cavity, rib, pocket, or internal form that a shaped electrode can reach from one side. Cobalt Chrome is electrically conductive and the final route follows the feature geometry and supplied condition.
What controls Sinker EDM on Cobalt Chrome?
The main process controls are electrode material, wear compensation, cavity depth, rib width, orbit strategy, debris evacuation, and rough-versus-finish electrodes. The Cobalt Chrome condition adds dimensional-stability and surface-integrity requirements.
What is the main risk?
For Sinker EDM, brittle edge behavior and fatigue-critical surfaces make recast and microcrack review important. Orbit, local heating and electrode wear can shift wall size while dishing the floor as roughing transitions to final orbit and floor sizing, especially around wear, medical and cyclically loaded edge features. The practical failure in Cobalt Chrome is local cracking and floor-size error in a wear- or medical-critical cavity. For Cobalt Chrome, use conservative energy, protect sharp edges and define microscopic surface-integrity acceptance where service life depends on it. Inspect wall size, floor depth and corner condition as separate acceptance items; document geometry, edge continuity and microscopic fatigue-critical damage for Cobalt Chrome.
What should I send for review?
Send the drawing, exact Cobalt Chrome condition, controlled geometry, tolerance, functional surface requirements, quantity, and inspection expectations. If any item is undecided, send what you have and we will help complete the review.