Process & Material
Beryllium Copper Wire EDM Feasibility Review
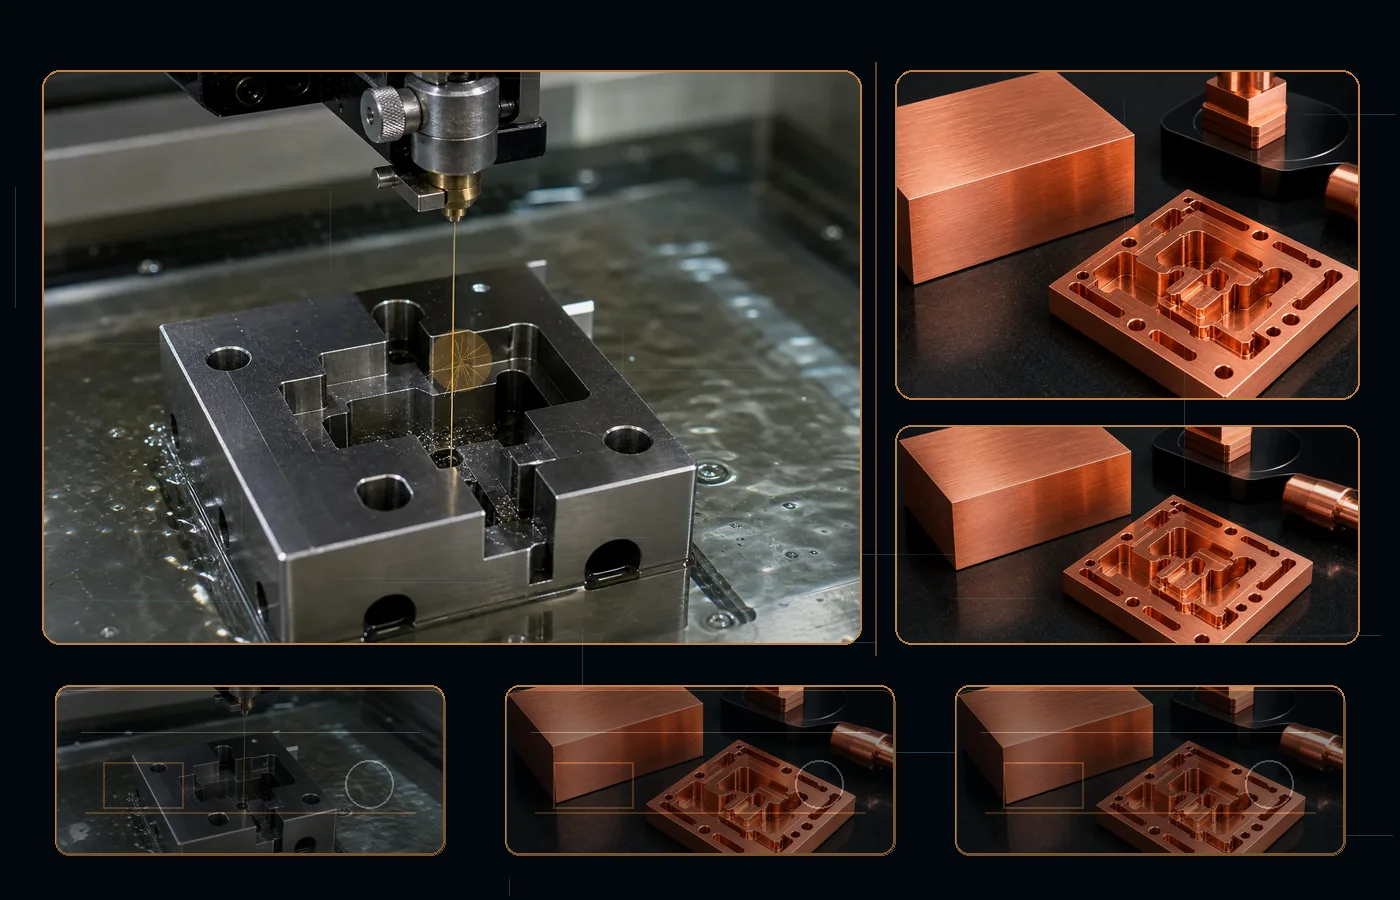
Beryllium Copper can be machined with Wire EDM when the geometry matches through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls. Beryllium Copper is age-hardenable copper alloy used for conductive spring and tooling features; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Wire EDM is suitable for Beryllium Copper when the wire can pass completely through the workpiece from an edge or a start hole. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
Age-hardenable copper alloy used for conductive spring and tooling features. In Wire EDM, the supplied condition changes stress release during the through cut, edge response to trim passes, and the final corrosion or surface-protection route.
Choosing the Right Condition
Choose Wire EDM for through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls. State the exact Beryllium Copper condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Wire EDM, heat-treatment condition and safe downstream handling must be identified. Guide alignment, flushing and residual restraint can produce a top-to-bottom mismatch when the slug, insert or thin ligament is finally separated; acceptance must focus on spring features, contact faces and post-aging geometry. On Beryllium Copper, the resulting defect can be profile movement, contact-edge alteration or spring-force loss after a thin feature is released. For Beryllium Copper, identify the temper and heat-treatment sequence, support compliant features, and protect contact or spring surfaces during finishing. Inspect both cut edges and confirm the final profile after support tabs are removed; document geometry, spring or contact function, recast and plating interfaces for Beryllium Copper.
How Wire EDM Works on Beryllium Copper
Wire EDM removes Beryllium Copper along a continuous through-cut with a moving wire electrode. Wire tension, guide alignment, flushing and trim-pass offset control kerf, taper, verticality and internal corner radius as the profile opens. The route requires a complete wire path from an edge or start hole and does not produce blind cavities.
Wire EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls |
| Tolerance | ±0.005–0.025 mm |
| Surface finish | Ra 0.2–3.2 μm |
| Wire diameter | 0.10–0.30 mm planning range |
| Minimum internal corner | Approximately wire radius plus spark gap |
| Main limitation | Blind cavities and closed pockets are not wire-cut features. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| solution annealed | Use gentle fixturing and adjust energy for high conductivity. | Soft edges can mark or roll under poor support. | Keep contact, bearing, and cosmetic faces as separate finish requirements. |
| cold-worked | Balance work-hardening stress with wear compensation. | Thin sections can move and micro features can round as electrodes wear. | Inspect edge radius and functional texture. |
| age-hardened | Use conservative finishing on hard-drawn or aged stock. | Over-finishing can remove useful texture or shift contact dimensions. | Apply finishing only to functional faces. |
How This Material Behaves
Beryllium copper changes markedly between solution-treated and age-hardened conditions. In EDM, this means hardness, springback, residual stress, and contact-surface behavior depend on the exact temper, while a thermally altered layer can reduce fatigue or electrical performance. State the alloy and age condition, support spring features, and keep recast, cleanliness, and plating requirements separate from Ra. For Wire EDM, heat-treatment condition and safe downstream handling must be identified. On thin conductive profiles, rapid heat flow and soft edges make support, wire offset and handling more important than nominal machinability.
Surface Integrity and Post-Process
For Wire EDM on Beryllium Copper, use gentle fixturing and a finish strategy that protects contact, sealing or heat-transfer surfaces. Separate the rough cut from skim cuts and apply the fine finish only to functional edges. Inspect roughness, edge rounding, recast and corrosion or fatigue requirements after the final pass; include polishing, coating or protection allowance wherever it changes final size.
Beryllium Copper Wire EDM Checkpoints
- Confirm that the feature matches through profiles, precision slots, punches, inserts, cutouts, narrow webs, and tapered walls.
- State the supplied condition: solution annealed, cold-worked, and age-hardened.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- electrical contacts
- electrodes
- busbar details
- punches and die inserts
- precision profile gauges
- gear and spline outlines
Limits and Better Alternatives
Main Limit
Blind cavities and closed pockets are not wire-cut features because the wire needs a continuous through path. On Beryllium Copper, heat-treatment condition and safe downstream handling must be identified; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use Sinker EDM for blind cavities, CNC machining for accessible open geometry, or laser cutting when thin-sheet speed matters more than EDM edge quality.
Practical Next Step
Send the Beryllium Copper drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Wire EDM with the adjacent EDM or conventional process.
Practical Takeaway
Beryllium Copper is compatible with Wire EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Additional Project Information
Include application, destination and end-use notes together with the material, quantity and drawing requirements.
Project Details for Technical Review
Include application and end-use notes when they affect material, inspection, documentation, or export review.
- Process: Wire EDM
- Material: Beryllium Copper
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.
Frequently Asked Questions
Can Beryllium Copper be machined with Wire EDM?
Yes, when the wire can pass completely through the workpiece from an edge or a start hole. Beryllium Copper is electrically conductive and the final route follows the feature geometry and supplied condition.
What controls Wire EDM on Beryllium Copper?
The main process controls are wire diameter, kerf compensation, flushing, wire tension, guide alignment, taper control, and trim-pass stability. The Beryllium Copper condition adds dimensional-stability and surface-integrity requirements.
What is the main risk?
For Wire EDM, heat-treatment condition and safe downstream handling must be identified. Guide alignment, flushing and residual restraint can produce a top-to-bottom mismatch when the slug, insert or thin ligament is finally separated; acceptance must focus on spring features, contact faces and post-aging geometry. On Beryllium Copper, the resulting defect can be profile movement, contact-edge alteration or spring-force loss after a thin feature is released. For Beryllium Copper, identify the temper and heat-treatment sequence, support compliant features, and protect contact or spring surfaces during finishing. Inspect both cut edges and confirm the final profile after support tabs are removed; document geometry, spring or contact function, recast and plating interfaces for Beryllium Copper.
What should I send for review?
Send the drawing, exact Beryllium Copper condition, controlled geometry, tolerance, functional surface requirements, quantity, and inspection expectations. If any item is undecided, send what you have and we will help complete the review.