Process & Material
AZ31 Magnesium Alloy Sinker EDM Feasibility Review
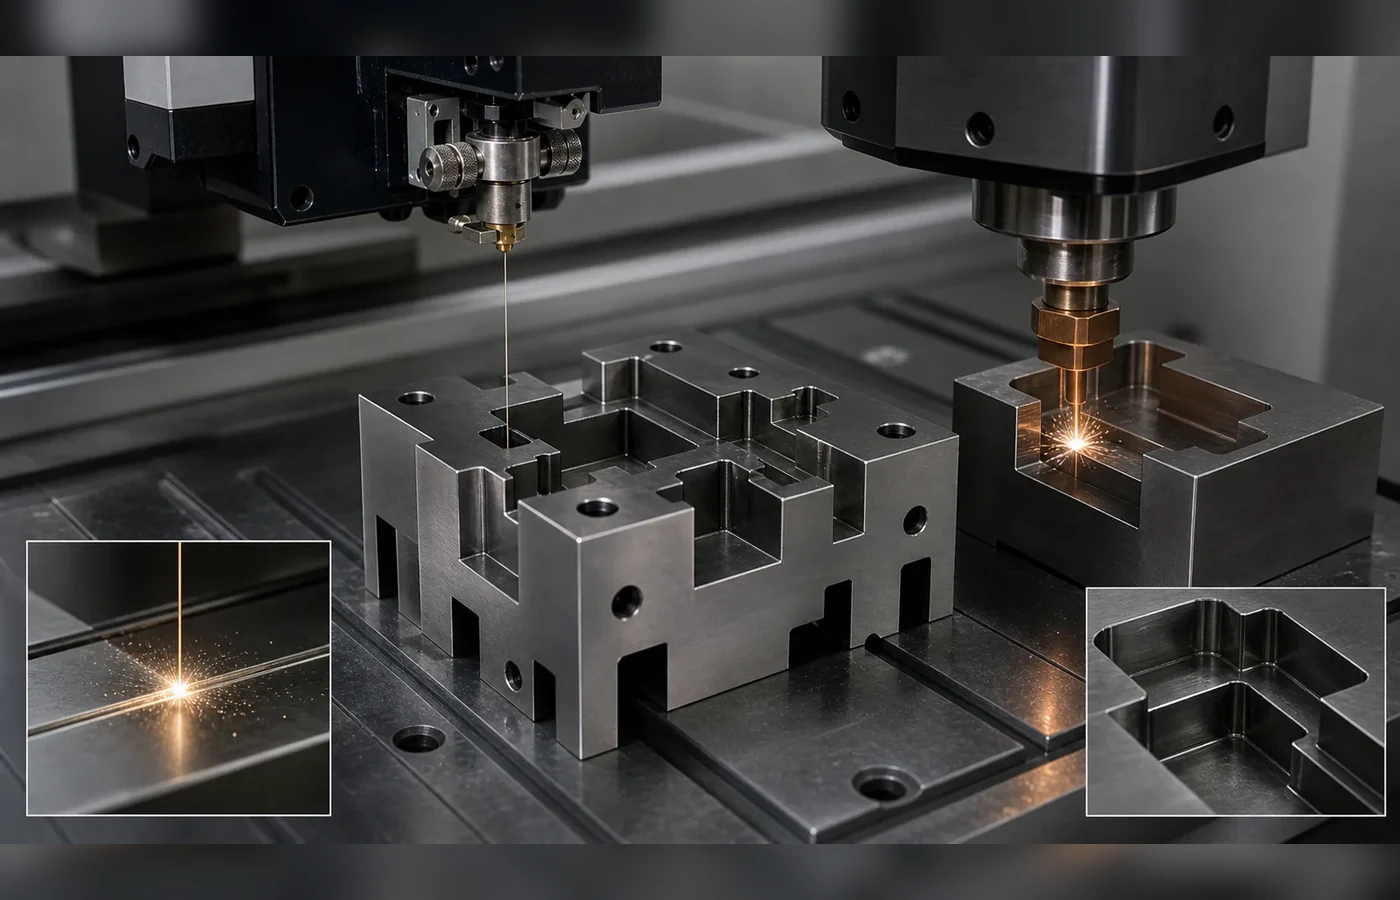
AZ31 Magnesium Alloy can be machined with Sinker EDM when the geometry matches blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach. AZ31 Magnesium Alloy is a wrought magnesium alloy with low density, low stiffness and strong sensitivity to thin-section support; the supplied condition affects support, discharge energy, finishing, and inspection.
Quick Answer
Sinker EDM is suitable for AZ31 Magnesium Alloy when the feature is a blind cavity, rib, pocket, or internal form that a shaped electrode can reach from one side. The supplied condition must be stated before tolerance and surface requirements are confirmed.
Key Material Decisions
How This Material Behaves
A wrought magnesium alloy with low density, low stiffness and strong sensitivity to thin-section support. In Sinker EDM, the supplied condition changes electrode wear, cavity-floor consistency, corner growth, and the finishing strategy—especially on deep ribs and textured surfaces.
Choosing the Right Condition
Choose Sinker EDM for blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach. State the exact AZ31 Magnesium Alloy condition, then set tolerance, finish, support, and inspection from the controlled feature rather than the whole part.
Risks to Manage
For Sinker EDM, soft thin stock can deform easily and all handling and post-process work must account for magnesium reactivity. Where debris collects at a cavity root or sharp internal corner, debris retention and electrode wear can change the root, wall and floor at different rates, with the highest consequence at reactive debris zones, weak exit edges and fresh surfaces. The AZ31 Magnesium Alloy feature may therefore show an unstable cavity burn, porous edge or finish variation where reactive debris accumulates. For AZ31 Magnesium Alloy, use a fully controlled machine-approved process, maintain debris evacuation and clean and protect the part immediately after cutting. Qualify the finish electrode on the actual cavity depth and flushing path; document geometry, debris-related surface damage and post-cut protection for AZ31 Magnesium Alloy.
How Sinker EDM Works on AZ31 Magnesium Alloy
Sinker EDM reproduces a shaped electrode as a blind cavity in AZ31 Magnesium Alloy. Electrode material, wear, orbit, pulse energy and debris evacuation control wall size, floor depth, corner definition and surface condition. Where final size or texture is critical, roughing and finishing electrodes should be planned as separate operations.
Sinker EDM Capability Reference
| What you're asking | What you can expect |
|---|---|
| Feature types | blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach |
| Tolerance | ±0.008–0.030 mm |
| Surface finish | Ra 0.2–6.3 μm |
| Electrode choice | Graphite or copper selected from cavity, finish, and wear needs |
| Primary cavity limit | Depth, rib width, access, and debris evacuation |
| Main limitation | Electrode access and debris evacuation limit deep, narrow blind geometry. |
Material Condition Reference
| Condition | What to expect | Watch out for | Surface notes |
|---|---|---|---|
| annealed wrought condition | Use stable support and economical roughing. | Clamping and material condition can move delicate features. | Apply fine finishing only to functional faces. |
| H24 work-hardened | Balance dimensional stability with feature-specific finishing. | Residual stress can shift thin sections or small details. | Identify wear, seal, fatigue, or contact surfaces. |
| formed and stress-relieved | Use conservative energy and selective inspection. | Finished or hardened surfaces can be sensitive to edge damage and recast. | Use lower-energy finishing or post-processing where function requires it. |
How This Material Behaves
AZ31 magnesium is light, soft, and chemically reactive. In EDM, this means low melting behavior and reactive debris demand a stable submerged process, while thin sections are easily marked or distorted by fixturing and flushing. Use machine-approved dielectric and fire-control settings, support the part continuously, and clean and protect fresh surfaces immediately after machining. For Sinker EDM, soft thin stock can deform easily and all handling and post-process work must account for magnesium reactivity. In blind cavities, debris evacuation and machine-approved dielectric control are essential because local accumulation can destabilize both finish and safe operation.
Surface Integrity and Post-Process
For Sinker EDM on AZ31 Magnesium Alloy, avoid unsupported absolute capability claims and define cleaning, residue and handling requirements before production. Use roughing and finishing electrodes separately where cavity size or texture is controlled. Apply polishing, lapping or recast removal only to named functional faces, and inspect wall, floor and corner condition after the final surface operation.
AZ31 Magnesium Alloy Sinker EDM Checkpoints
- Confirm that the feature matches blind cavities, ribs, shaped pockets, mold details, deep forms, and internal geometry that a traveling wire cannot reach.
- State the supplied condition: annealed wrought condition, H24 work-hardened, and formed and stress-relieved.
- Mark the controlled dimensions, functional surfaces, datum scheme, and inspection method.
Typical Parts and Features
- lightweight prototypes
- instrument frames
- special fixtures
- mold cavities
- blind pockets
- deep ribs
Limits and Better Alternatives
Main Limit
Electrode access and debris evacuation limit deep, narrow blind geometry. On AZ31 Magnesium Alloy, soft thin stock can deform easily and all handling and post-process work must account for magnesium reactivity; the supplied condition still controls support, finishing, and surface-integrity review.
Consider Another Route When
Use Wire EDM for through profiles, CNC machining for open cavities with tool access, or grinding for simple flat precision surfaces.
Practical Next Step
Send the AZ31 Magnesium Alloy drawing with condition, controlled geometry, tolerance, functional surface callouts, quantity, and inspection requirements. If the route is unclear, we will compare Sinker EDM with the adjacent EDM or conventional process.
Practical Takeaway
AZ31 Magnesium Alloy is compatible with Sinker EDM when the feature matches the process access. The supplied condition determines support, finishing, surface control, and inspection.
Additional Project Information
Include application, destination and end-use notes together with the material, quantity and drawing requirements.
Project Details for Technical Review
Include application and end-use notes when they affect material, inspection, documentation, or export review.
- Process: Sinker EDM
- Material: AZ31 Magnesium Alloy
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.