Application Review
Mold & Die EDM Machining for Tungsten Carbide
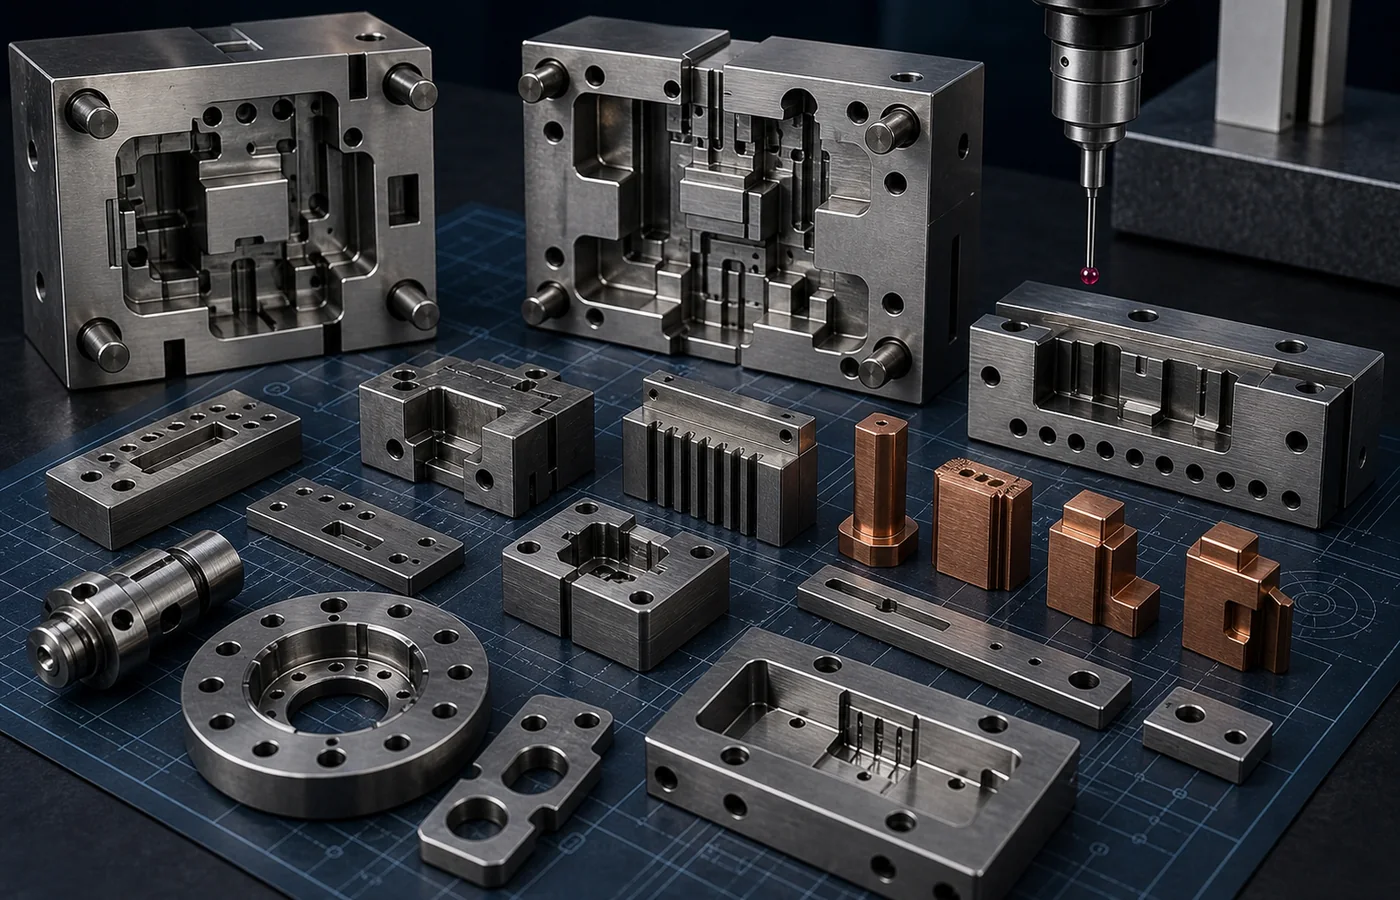
Tungsten Carbide can be reviewed for Mold & Die, but the exact role of the part must justify the material’s strength, corrosion, wear, thermal, and documentation characteristics. In Mold & Die, the functional requirements are sharp internal geometry, controlled clearance, wear surfaces and repeatable insert fit. The material-specific concerns are that edge chipping and microcracks matter more than nominal bulk hardness.
Quick Answer
Tungsten Carbide can be considered for Mold & Die, but first confirm that its strength, corrosion, wear, thermal, and documentation profile fits the actual part. Route each feature to Wire, Sinker, Small Hole, or Micro EDM from its access geometry.
Key Application Decisions
What's at Stake
In Mold & Die, the part fails when incorrect corner radius, heat-treatment movement or unsuitable texture on molding and cutting faces. Tungsten Carbide is hard, brittle composite whose binder content affects conductivity and fracture behavior; its role must be justified by the actual load, environment, wear, temperature, corrosion, or contact requirement.
How to Get It Right
Use Tungsten Carbide only where its properties match the functional part. Route through profiles, blind forms, difficult holes, and miniature details to the appropriate EDM process, then define profile, cavity, hardness, surface finish. Compare the material with the alternatives listed below before freezing the drawing.
What Can Go Wrong
If grade, condition, or functional face is not controlled, brittle edges, binder loss, chipping, and specialized metrology limit general structural use can defeat the application requirement for wear, polishability, heat treatment, rib geometry, and production volume. A technically successful EDM cut does not correct a poor material choice. Keep Tungsten Carbide within this permitted role: wear inserts, nozzles, micro-orifice parts, high-temperature contacts, and refractory features.
How EDM Fits the Application
EDM is selected feature by feature for Mold & Die: Wire for through profiles, Sinker for blind forms, Small Hole for difficult holes, and Micro EDM for miniature details. On Tungsten Carbide, the supplied condition determines support, finishing energy, post-processing, and inspection.
Tungsten Carbide Application Reference
| What matters | What to expect |
|---|---|
| Material behavior | hard, brittle composite whose binder content affects conductivity and fracture behavior |
| Material-specific concern | edge chipping and microcracks matter more than nominal bulk hardness |
| Surface action | use conservative energy, strong support and inspection focused on edge chipping and subsurface damage |
Mold & Die Application Planning
| What matters | What to expect |
|---|---|
| Typical parts | punches, die inserts, mold cavities, and slides and lifters |
| Functional requirement | sharp internal geometry, controlled clearance, wear surfaces and repeatable insert fit |
| Main failure risk | incorrect corner radius, heat-treatment movement or unsuitable texture on molding and cutting faces |
| Inspection focus | profile, cavity, hardness, surface finish |
| Planning context | Working clearances and insert fits are commonly planned in the ±0.005–0.020 mm range, with finish selected by wear, release and polishing requirements. |
Material Choices for This Application
Tungsten Carbide is a direct option for Mold & Die when the part benefits from wear resistance, high-temperature capability, or refractory performance. Its main limitation is brittle edges, binder loss, chipping, and specialized metrology limit general structural use, so the EDM plan must connect the exact condition to wear, polishability, heat treatment, rib geometry, and production volume. Use it on roles that need those properties rather than selecting it only because it is conductive. Consider these alternatives where the current material does not fit the functional role: A2 / D2 / DC53 fits wear-dominant punches and inserts; brittle edges and hardened-condition recast need control; H13 fits hot-work molds and thermally cycled inserts; thermal fatigue and heat-treatment condition dominate; P20 fits general mold cavities and bases; not the best choice for the highest wear edges; 420 stainless fits corrosion-resistant polished molds; polishing and passivation route must be planned.
Functional Surface and Edge Control
Mark the Mold & Die edges, contact, seal, wear, alignment, or cosmetic faces that carry the function. Inspect profile, cavity, hardness, surface finish separately. For Tungsten Carbide, manage the material-specific risks: Edge chipping and microcracks matter more than nominal bulk hardness. Do not approve the part from one broad Ra value.
Mold & Die Buyer Checkpoints
- Identify the feature whose failure would cause incorrect corner radius, heat-treatment movement or unsuitable texture on molding and cutting faces.
- State the exact Tungsten Carbide condition and define the datum and method for profile, cavity, hardness, surface finish.
- Send functional surface notes, quantity, drawing revision, and documentation needs before quotation.
Common Applications
- punches
- die inserts
- mold cavities
- slides and lifters
Limits and Better Alternatives
Main Limit
Tungsten Carbide compatibility does not select the EDM process or prove that the material is suitable for every Mold & Die function.
Consider Another Route When
Consider A2 Tool Steel, D2 Tool Steel, and H13 Tool Steel when their strength, corrosion, wear, temperature, or documentation profile fits the part better. Use conventional machining when the geometry is open and EDM adds no functional value.
Practical Next Step
For an EDM review of Mold & Die in Tungsten Carbide, send the drawing, exact condition, critical feature, tolerance, functional surfaces, quantity, and the inspection or documentation requirements. If the material choice is uncertain, we can compare it with a better-fitting alloy before quotation.
Practical Takeaway
Tungsten Carbide can be used for Mold & Die only where its material properties support the functional demand. Route each feature to the correct EDM process and release profile, cavity, hardness, surface finish with the functional surface requirements.
Additional Project Information
Include application, destination and end-use notes together with the material, quantity and drawing requirements.
Project Details for Technical Review
Include application and end-use notes when they affect material, inspection, documentation, or export review.
- Material: Tungsten Carbide
- Application: Mold & Die
- Drawing or part sketch
- Material grade
- Thickness / part size
- Quantity
- Tolerance and critical dimensions
- Surface finish or inspection requirement
STEP/STP, DXF, DWG, PDF, IGS/IGES or ZIP.
Confidential drawing review. NDA support available on request.